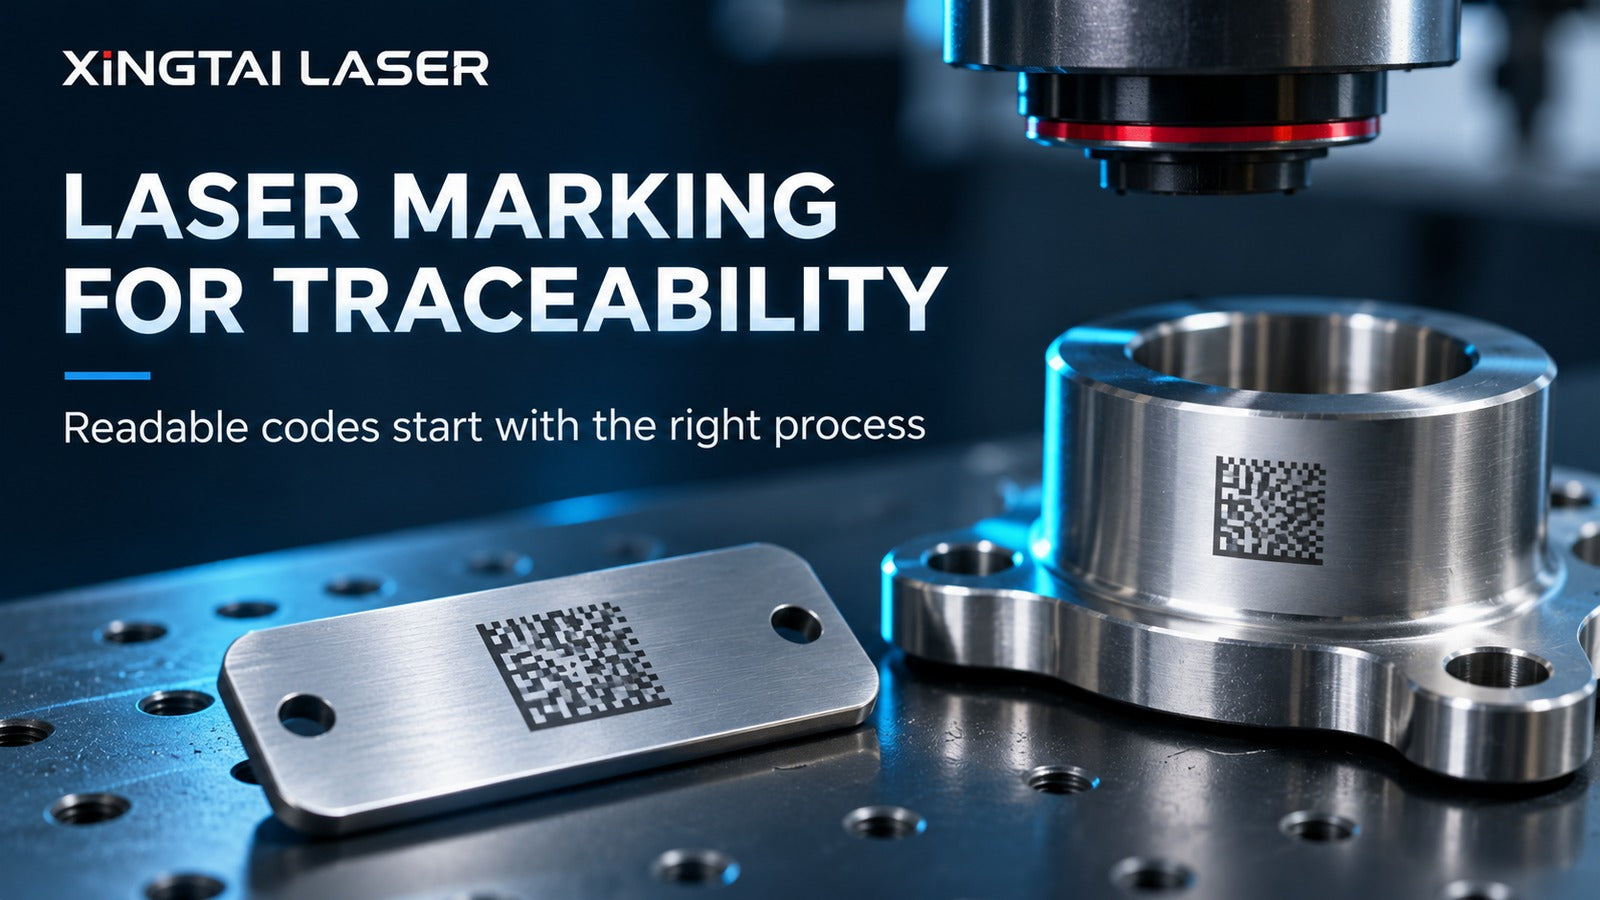
Laser Marking for Traceability: How to Make Data Matrix Codes That Stay Readable
Tjxtmachine | Application Guide | November 3, 2026
When a customer asks for a fiber laser marking machine, the first question is often about power: 20W, 30W or 50W? For manufacturers adding serial numbers or 2D codes to metal parts, a more useful first question is whether those marks will still be readable after handling, finishing and years of use.
A neat-looking code is not necessarily a reliable code. The scanner, lighting, surface finish, cell size and the information encoded can all affect the outcome. A part that scans once on a phone is not automatically ready for a production traceability program.
This is an application guide, not a report of a new machine launch. We reviewed manufacturing news from the past seven days, but found no sufficiently well-substantiated, distinct development that would add more customer value than a practical direct-part-marking guide. The technical references below are established standards and guidance, not news published this week.
1. Define What the Code Must Do
Before choosing a laser, decide what the code needs to identify. Is it a unique serial number, a production batch, a part number or a link to a service record? The answer affects the data format, symbol size and the system that generates and stores the information.
Data Matrix and QR Code are both two-dimensional symbols, but they are not interchangeable in every supply chain. A customer specification may require Data Matrix, a GS1 DataMatrix data structure, a particular scanner or a documented verification grade. A GS1 DataMatrix is not simply any square code; it has specific data-encoding rules.
The first equipment decision is a data and acceptance decision, not a wattage decision.
2. Select the Marking Surface Before the Machine
An identical laser program can produce different results on brushed stainless steel, polished stainless steel, anodized aluminum, painted metal and engineering plastic. Surface reflectivity, coating, texture and curvature all influence contrast and readability.
Choose a location that is reasonably flat, accessible to the intended reader and protected from expected wear. Avoid placing a code across an edge, a highly distorted surface, a sealing area or a position that will be covered during assembly unless the application explicitly permits it.
Test the actual production material and finish, not a convenient demonstration plate.

3. Match Laser Type and Marking Method to the Material
For many metal components, fiber laser marking is a sensible starting point. Depending on the material and settings, the process may create a contrasting surface mark or remove material to form an engraved mark. More depth is not always better: excessive roughness or distorted cells can reduce symbol readability.
For selected anodized-aluminum and stainless-steel applications where surface response or color control matters, a suitable JPT MOPA fiber laser may be evaluated. Tjxtmachine offers 60W and 100W JPT MOPA configurations, but a particular color or code grade must be proven on the customer’s sample.
If the job includes suitable non-metal materials or a mix of metal and non-metal parts, UV laser marking may deserve evaluation. For wood, leather or acrylic applications, CO₂ processing may be more appropriate. Material compatibility and marking results must be checked rather than inferred from laser type alone.
A good marking process preserves the part’s function while creating the required code contrast.

4. Design for Readability, Not Just Appearance
Code readability depends on the whole symbol: cell dimensions, quiet zone, contrast, geometry, surface condition and how the reader illuminates the mark. Packing too much data into a very small area can make production unnecessarily difficult.
Ask the customer which scanner or vision system will read the code and under what conditions. A code read at a desk may behave differently under factory lighting, after coating or when mounted on a curved component.
Do not set a universal minimum code size without testing the actual scanner, marking optics and part.
5. Keep the Workpiece Position Repeatable
When a part is marked repeatedly, stable positioning matters. A simple fixture can reduce variation in focus, rotation and the location of the code. For cylindrical parts, a rotary setup may be useful, but the usable marking geometry must be confirmed.
Choose the marking field to cover the real artwork and fixture layout; do not automatically select the largest field. A larger scan field may change optical conditions and the focused spot size, which can matter for small cells.
Before automating a marking station, establish a stable manual process and verify that the fixture and mark placement are repeatable.
6. Separate Scanning From Formal Verification
A successful scan tells you that one reader decoded a symbol under one set of conditions. It does not by itself establish that the symbol meets a customer’s quality specification.
For direct-part-marked symbols, ISO/IEC 29158:2025 provides a published quality test specification that modifies the methodology of ISO/IEC 15415 for DPM applications, including illumination and grading considerations. The applicable grade and inspection method must be agreed with the customer; not every job requires the same specification.
GS1 also states that GS1 DataMatrix quality should be assessed with an ISO/IEC-compliant verifier. A phone camera or an ordinary barcode reader is not a substitute for formal verification when a verified grade is required.
A readable code is the beginning of quality control; a verified code is evidence against a defined requirement.

7. Run a Production-Like Sample Test
For a meaningful sample test, send the real part, material grade, surface finish, drawing, required code content, intended symbol dimensions, expected production volume and scanner or verification specification.
Mark several samples using the proposed settings. Check the code at the beginning and end of the batch, under the intended lighting, and after any relevant cleaning, coating or handling steps. Where the application requires durability, agree on an appropriate test method rather than assuming permanence from appearance alone.
Record the approved settings, fixture arrangement, sample results and any failed reads. If the job is regulated or safety-critical, the customer’s qualified engineering and quality teams should define additional validation.
The best machine demonstration is a repeatable result on the customer’s own part, measured against the customer’s own acceptance criteria.
What Should Buyers Ask Tjxtmachine?
For a standard metal-part traceability inquiry, tell us the material and finish, code size, marking area, number of parts per shift, fixture requirements and how the finished code will be checked. A 20W or 30W fiber laser may be a starting point for many ordinary marking jobs, but the correct configuration depends on sample results.
If fine detail, anodized aluminum or specific surface effects are involved, we can discuss suitable MOPA or UV configurations where applicable. We do not claim that a standard marking machine includes a built-in ISO/IEC DPM verifier or automated quality grading. Scanners, verifiers, vision systems and software integration must be specified and validated separately.
Our recommendation is to select the marking process around the material, required data and inspection method—not to buy extra laser power before the application is understood.
Frequently Asked Questions
Is Data Matrix the same as QR Code? No. Both are 2D symbols, but customer specifications, data structures and reader requirements can differ.
Will any smartphone verify a laser-marked Data Matrix code? No. A successful decode is not the same as standards-based quality grading.
Is deeper engraving always more durable or easier to read? No. The effect depends on the material, environment, surface texture and scanner; excessive engraving can impair readability.
Can one machine mark both metal and plastic? Sometimes, but compatibility depends on the specific plastic and required result. UV marking may be worth evaluating for mixed-material applications.
Conclusion: Traceability Starts With a Verified Process
Permanent identification is valuable only when the right information remains accessible to the people and systems that need it. Define the data, select the surface, test the laser process and verify the result.
For small manufacturers, a well-designed fixture, realistic sample testing and clear acceptance criteria can be more useful than an expensive machine configuration chosen without an application plan.
The goal is not simply to make a code. It is to make the right code readable, repeatable and useful throughout the product’s life.
Technical References and Transparency
This article is an evergreen application guide, not a claim of breaking industry news. GS1 provides barcode application guidance; ISO publishes the DPM quality test specification. Tjxtmachine does not claim that its standard marking equipment includes a DPM verifier. Illustrations are conceptual, and depicted codes are not verified production marks.
-
Publicado en
Data Matrix, direct part marking, fiber laser marking, laser marking, traceability