Fiber Laser Cutting Lens Maintenance: 7 Checks to Prevent Poor Cut Quality
Tjxtmachine | Practical Maintenance Guide | November 6, 2026
A cutting program that worked yesterday can suddenly produce burrs, uneven edges or incomplete cuts today. Increasing power or slowing the machine is tempting, but a contaminated protective window, a damaged optical surface or a change in gas delivery may be the real cause. Before changing process settings, inspect the cutting head and maintenance history systematically. This is a practical maintenance guide, not an announcement of a new machine. Always follow the manual for the installed cutting head; optical assemblies differ, and sealed modules must not be opened by unauthorized personnel.
1. Record the symptom before changing settings
Record the material, thickness, assist gas, nozzle, cutting program, shift and date. Photograph the edge and compare it with an approved sample. Is the problem across the whole sheet or only in corners? Does it occur on one material but not another? This log helps distinguish a process problem from a machine problem. A consistent test coupon is more useful than random adjustments to power and speed.
2. Inspect the protective window without touching the optical surface
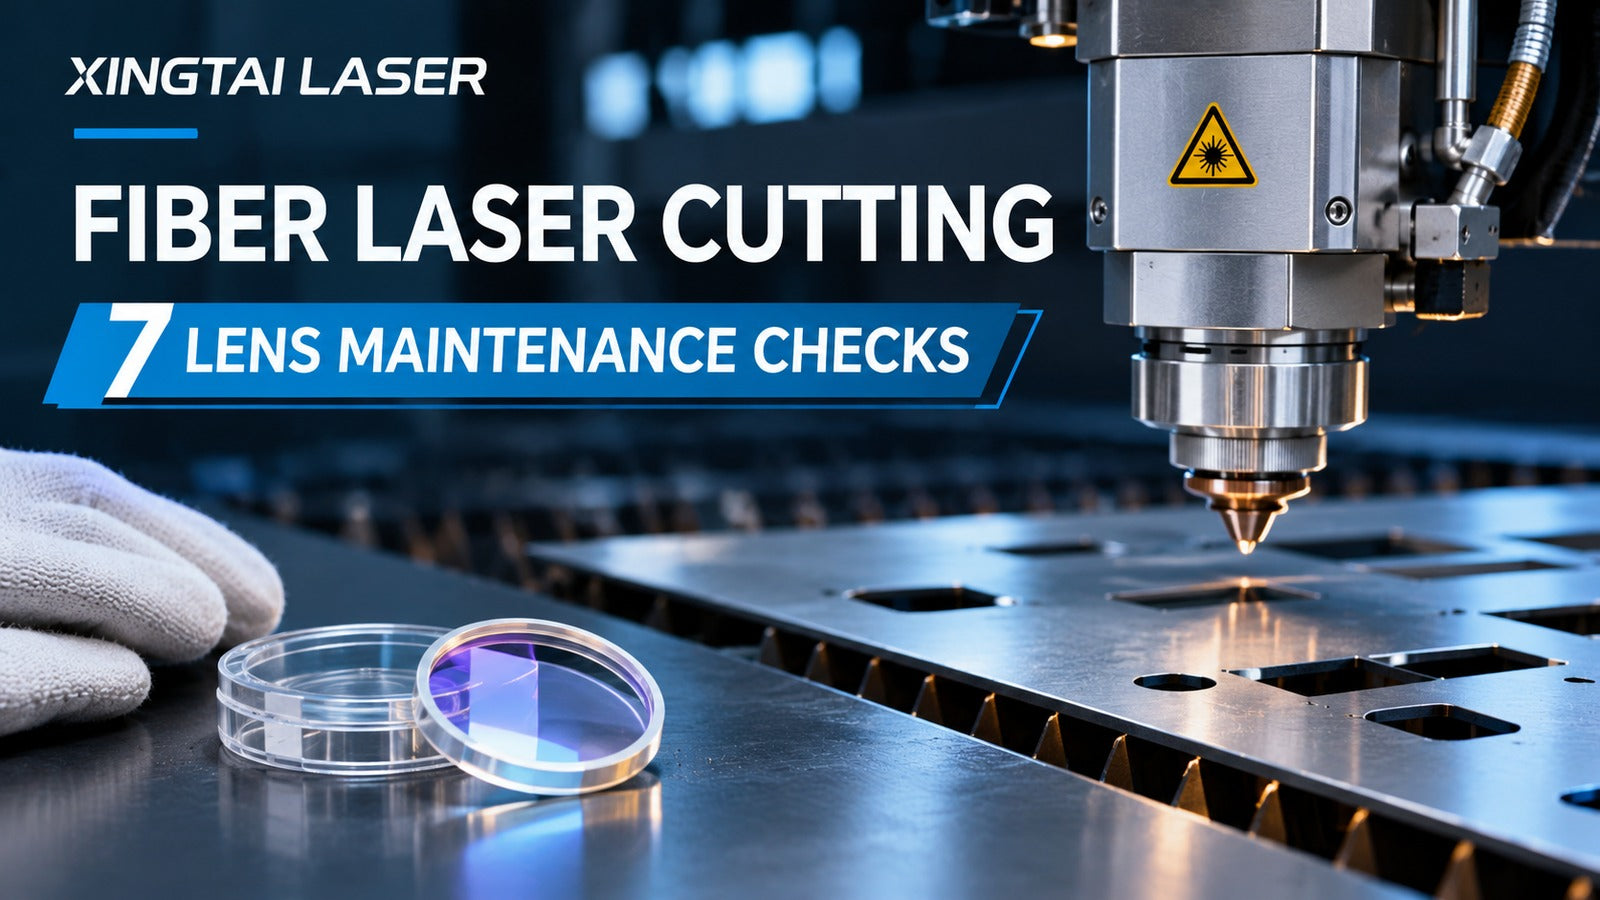
The protective window helps shield more sensitive optics from spatter and contamination. Following the manufacturer's safe shutdown and inspection procedure, look for haze, particles, discoloration, coating damage and burn marks. A window that looks almost clean may still affect beam transmission. Do not wipe optical surfaces with a shop rag or bare fingers. Inspect the protective window in good light and compare it with an approved clean reference.

3. Follow the specified cleaning procedure—or replace the window
Not every lens or coating tolerates the same solvent, wipe or disassembly method. Use only the consumables and cleaning sequence specified for the installed optical assembly. Keep clean optics covered, work in a low-dust area and avoid touching coated faces. If there is permanent staining, pitting, coating damage or uncertainty about safe cleaning, stop and request the approved replacement procedure. Never use improvised abrasives.
4. Check the nozzle and cutting-head consumables
An off-center nozzle, spatter buildup, damaged tip or incorrect standoff can cause inconsistent gas flow and edge quality. Inspect the nozzle only after the system is made safe. Compare nozzle condition and size with the approved process sheet, and use the cutting-head manufacturer's centering and calibration instructions where applicable. Do not assume every cutting problem originates in the lens.
5. Verify assist-gas delivery and air quality
Gas pressure at the supply is not necessarily the pressure reaching the cutting zone. Check for leaks, blocked filters, moisture, incorrect gas selection and inconsistent delivery according to the machine manual. Poor air or gas quality may contribute to contamination and cut defects. Gas and ventilation requirements differ by material; confirm the applicable process specification before production.

6. Compare focus and cut quality using a controlled sample
After an authorized maintenance intervention, run the same approved test part with the same material, thickness, gas and settings. Record edge quality, dross, kerf consistency and any alarms. If focus calibration is required, use the manufacturer-approved method and trained staff. Avoid compensating for a damaged optical component by repeatedly increasing power. Compare the post-maintenance sample with the original approved part before restarting a full batch.
7. Create a practical maintenance record
A useful log includes inspection date, operator, optical part identification, observed condition, action taken and the next review. Maintenance intervals should reflect material, duty cycle, fume and spatter exposure—not a universal promise that every lens lasts a fixed number of hours. Keep spare approved consumables protected from dust and moisture.

Quick troubleshooting checklist
If the cut suddenly deteriorates, record the symptom; confirm the job settings; inspect accessible protective optics and the nozzle; check gas delivery and extraction; review recent maintenance; and run a controlled sample. Escalate to qualified service personnel if the issue persists or requires opening protected optical assemblies.
Frequently asked questions
Should I clean the protective lens every day? Inspect according to the manufacturer's schedule and the actual contamination level. Clean only when indicated and with the approved method; unnecessary handling can itself cause damage.
Can a dirty lens cause burrs? Optical contamination can contribute to unstable cutting, but burrs also have other possible causes, including focus, gas, nozzle condition and process settings.
Can I use alcohol on any laser lens? No. Cleaning agents and coatings vary. Follow the specific optic manufacturer's instructions.
Does this guide apply to every Tjxtmachine machine? No. It is intended for relevant fiber laser cutting systems. Marking, welding, cleaning and other laser systems can use different optical layouts.
Conclusion
Stable cutting begins with repeatable process conditions and disciplined inspection—not simply more laser power. For a useful equipment or after-sales discussion, send Tjxtmachine your machine model, cutting-head model, material and thickness, current process settings, photos of the cut edge and any alarm messages. That information helps narrow the next diagnostic step without guessing.
Editorial note and technical sources
This evergreen application guide is not a report of a new Tjxtmachine product or a claim that all Tjxtmachine machines use the same cutting head. Technical background: Mate Precision Technologies: Contaminants Reduce Lens Life; Trotec Laser: How to Clean Laser Focus Lenses; OMTech: How Should I Clean the Focal Lens?. These references describe equipment-specific approaches; follow the actual installed equipment manual.
-
Publicado en
fiber laser cutting, laser cutting troubleshooting, lens maintenance